
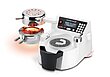

MINISTAR S®
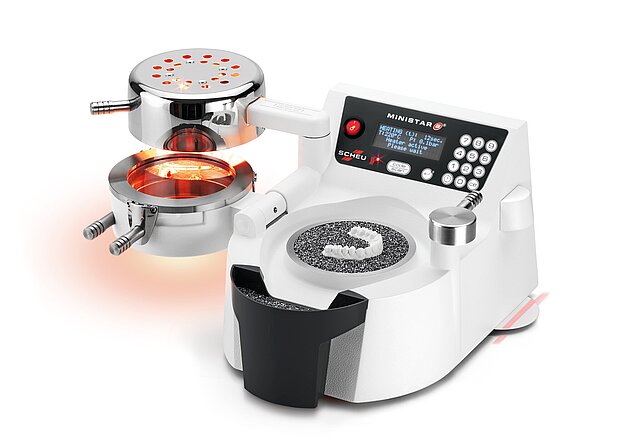
The compact pressure moulding device MINISTAR S® with scanning technology: the scanner reads the coded thermoforming foil and all important parameters such as heating time, temperature and cooling time are programmed automatically. Combined with the ultra-fast, patented heater and the high operating pressure of up to 4 bar, which can be adjusted via a pressure regulator on the device, precise thermoforming results are achieved in record time. Equipped with a user-friendly membrane keypad and a large display which indicates and monitors all operating parameters.
Technical data:
Voltage/Power: 230/115/100 V, 750 W
Working pressure: 0.5–4.0 bar
Dimensions (W x H x D): 500 x 210 x 400 mm
Weight: 9 kg
3-year warranty, 10-year availability of spare parts
Call and order directly: +49 2374 9288-0 Monday - Thursday 07:45 - 16:30, Fri. 07:45 - 14:00
More information
- Guideline to solve technical problems with BIOSTAR IV-VII, MINISTAR®, MINISTAR S®, TWINSTAR®
- Indication chart on applications in the pressure moulding technique
- Operation manual MINISTAR S®
- Sales folder MINISTAR S®
- Instruction for mounting the impact plate for BIOSTAR® / MINISTAR S®
- Overview on pressure moulding material
- Comparison_BIOSTAR_MINISTAR_B4A_GB
- Drill for decompression BIOSTAR®, MINISTAR S®, TWINSTAR® P
- MINISTAR S®_Black-Edition_Sales Folder_GB
- Catalogue Pressure Moulding Technique
- Video training: How to install and start up MINISTAR S®
- Video training: How to fabricate an occlusal splint using DURASOFT®
- Video training: How to fabricate an individual sports mouth guard
- Device- registration
FAQ
No, you can only process material with a diameter of 125 mm in SCHEU-DENTAL pressure moulding machines. Make sure to use the correct material size to avoid any problems during pressure build-up. The rim of a too small blank gets pulled out from the clamping of balancing and locking ring. Thus, a precise and correct thermoforming result is not ensured.
Maybe there is a pellet on the edge of the model cup between material and clamping ring. Interrupt the thermoforming process, taking care the model cup rim is absolutely clean before closing the pressure chamber.
Leaking of air usually does not affect the thermoforming result, because the compressor is constantly supplying air. Nevertheless, you should check the following:
When working on the model platform,
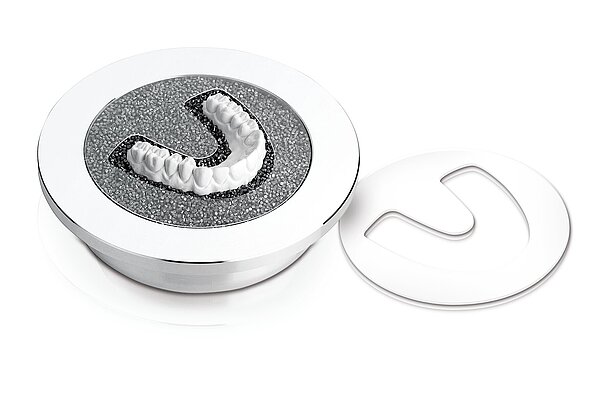
ensure the model is placed flush with the surface of the model platform. If it's not, trim the model flat or embed it into the pellets.
sharp edges may have damaged or torn the material. If this is the case, remove the sharp edges on the model.
the material may have moved when being clamped. In this case, clamp a new blank and restart the thermoforming process.
the balancing ring may have got stuck. In this case, remove the balancing ring, clean, grease and reinsert it. Ensure it is freely movable!
When embedding the model into the pellets, sharp model edges may cause perforation mainly of thin material.
No, this is not possible. However, depending on the series of your pressure moulding device, you can set an individual heating time using the “clock” symbol on the keyboard of your device or by using the “+” and “-” buttons. Please refer to the manual of your device to find out which option applies to your device. The operation manual of the current series of our pressure moulding machines can be found on this site under "Further Information" for download. Operation manuals of previous device series are available under SERVICE on top of this web site.